

What this industry manufactures
Hand lay-up is used across most categories of general-purpose FRP product — water tanks, cooling tower panels, roofing sheets, door skins, general panels and moulded items are all commonly built this way. Rather than being tied to one product category, it's the fabrication method that underlies most general-purpose FRP manufacturing in a typical workshop.
Why GP Yellow Resin is suitable
What every hand lay-up job has in common is a fabricator working resin into reinforcement by hand, layer by layer. GP Yellow Resin's 450–600 cPs body is thicker than GP Clear Resin's 350–450 cPs, which asks a little more of the roller to drive it fully through the fibre without dragging, but its longer 10–15 minute gel time gives fabricators more time to complete each layer by hand before it begins to set — a workable trade-off for hand lay-up specifically, since the technique already relies on manual working time rather than machine metering. It is not a better resin for this process than GP Clear Resin, simply a slower-gelling one with a yellow tint instead of being colourless.
Required resin characteristics
- 01A viscosity workable under a brush or roller, even if thicker than a low-viscosity laminating grade
- 02Even wet-out through reinforcement without leaving dry fibres or resin-rich pockets
- 03A gel time long enough to complete a layer by hand, without an excessively long production cycle
- 04Reliable room-temperature cure with no special equipment required
- 05Predictable behaviour across different ambient workshop temperatures
Manufacturing process
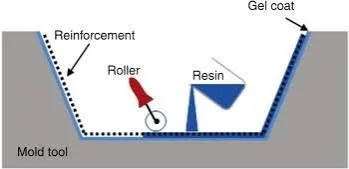
In hand lay-up, chopped strand mat or woven roving is placed into or against a mould, and GP Yellow Resin, catalysed with an MEKP hardener and cobalt octoate accelerator, is applied by brush or poured on and worked through the reinforcement with a laminating roller — its thicker body needs a slightly firmer rolling pass than a low-viscosity grade to drive it fully through the fibre. Additional layers are built up the same way until the required thickness is reached, then the part cures at room temperature before being released from the mould.
Advantages
- Longer 10–15 minute gel time gives fabricators more working time to complete a hand-applied layer
- Same non-accelerated MEKP/cobalt octoate cure system as GP Clear Resin
- Workable under standard brush or roller application
- Consistent 99% purity keeps hand-applied laminate quality uniform batch to batch
Common products produced
- Water tanks, cooling tower panels and roofing sheets
- Door skins and general FRP panels
- Moulded FRP parts across most general-purpose applications
Frequently asked questions
Its 450–600 cPs viscosity is thicker than a low-viscosity laminating grade, so it needs a firmer rolling pass to drive fully through reinforcement, but its 10–15 minute gel time gives fabricators more working time to complete a layer by hand before it sets.
GP Clear Resin's lower 350–450 cPs viscosity is somewhat easier to spread under a roller. GP Yellow Resin is still workable by hand lay-up, just with slightly more rolling effort to avoid dry patches — its longer gel time offsets some of that by giving more time to do it.
It is cured at room temperature with an MEKP catalyst (around 1.5%) and a cobalt octoate accelerator (0.3–0.5%), with dosage commonly adjusted to suit ambient workshop temperature and the size of the part being laminated.
Yes. GP Yellow Resin wets out both, and many hand lay-up jobs combine chopped strand mat for bulk with woven roving where extra structural strength is needed.
This depends on the part's required thickness and the resin's gel time. Its longer 10–15 minute gel time gives a bit more room to complete a layer before moving on, but the overall approach is the same as with GP Clear Resin: wet out and roll one layer before adding the next.
Need GP Yellow Resin for your hand lay-up production?
Get a bulk quote for GP Yellow Resin, or talk to our technical team about whether GP Yellow Resin or GP Clear Resin better suits your lay-up process.