

What this industry manufactures
Spray-up is used for products where higher-volume production and moderate part complexity make chopper-gun application worthwhile — water tanks, bathtubs and sanitaryware, panels, cooling tower components and similar moulded shapes with large surface areas benefit most from the process's speed advantage over manual lay-up.
Why GP Clear Resin is suitable
Spray-up puts different demands on a resin than hand lay-up — it needs to atomise cleanly through spray equipment without clogging, and its gel time has to be predictable enough for an operator to build up thickness across a mould without the first pass gelling before the last one is sprayed. GP Clear Resin's 350–450 cPs viscosity is compatible with standard spray-up equipment, and because it's a non-accelerated resin, fabricators can dose the accelerator to set the gel time that best matches their equipment's spray rate and mould size.
Required resin characteristics
- 01A viscosity compatible with chopper-gun atomisation without clogging equipment
- 02Predictable gel timing that can be tuned to the spray rate and size of the mould
- 03Even resin distribution alongside chopped roving as it's deposited on the mould
- 04Reliable mechanical strength once the sprayed laminate is compacted and cured
- 05Consistent behaviour across repeated spray cycles in a production run
Manufacturing process
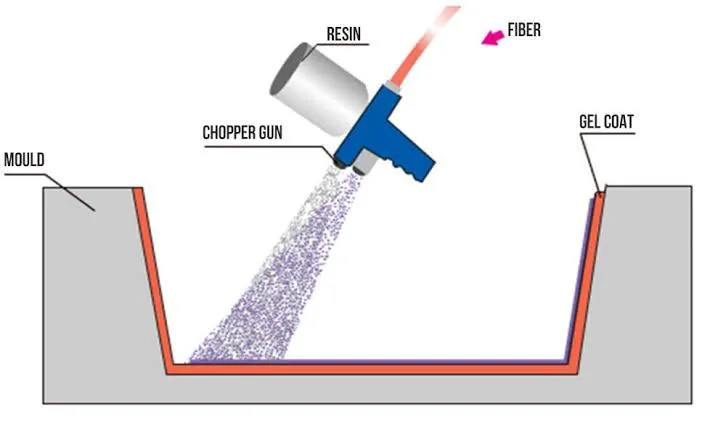
In spray-up, resin catalysed with an MEKP hardener and cobalt octoate accelerator is fed through a chopper gun alongside continuous glass roving, which is cut and deposited onto the mould simultaneously with the resin spray. The sprayed laminate is then compacted with a roller to remove air and ensure the resin has fully wet out the chopped glass fibre, in the same way a hand-applied layer would be rolled. Multiple passes build up the required thickness before the part cures at room temperature and is released from the mould.
Advantages
- Compatible viscosity for clean atomisation through standard spray-up equipment
- Non-accelerated cure system lets fabricators dial in gel time to match spray rate and mould size
- Sub-8-minute gel time supports faster cycle times than hand lay-up on larger parts
- Consistent 99% purity maintains laminate quality across high-volume spray production
Common products produced
- Water tanks and sanitaryware produced at volume
- Bathtubs and moulded bathroom fixtures
- Cooling tower panels and casings
- General FRP panels with large surface areas
Frequently asked questions
Yes, its viscosity is compatible with standard spray-up equipment. As with any resin, operators should check compatibility with their specific spray equipment setup and adjust accelerator dosage to suit.
Because spray-up deposits resin and reinforcement faster than hand lay-up, gel time is tuned to the operator's spray rate and the mould's size — enough time to complete all passes and roll out air, but not so long that production slows unnecessarily.
Spray-up uses continuous glass roving fed through the chopper gun and cut on application, rather than pre-cut chopped strand mat — but the resin's role in wetting out that reinforcement is the same.
It is cured at room temperature with an MEKP catalyst (around 1.5%) and a cobalt octoate accelerator (around 0.4%), with dosage adjusted to the operator's spray rate and the equipment being used.
Spray-up generally suits higher-volume production of moderately complex shapes where labour savings matter most; hand lay-up gives more control for complex geometries or lower-volume work. Both use the same GP Clear Resin.
Need resin for your spray-up production?
Get a bulk quote or talk to our technical team about the right grade and dosage for your spray-up process.