

What this industry manufactures
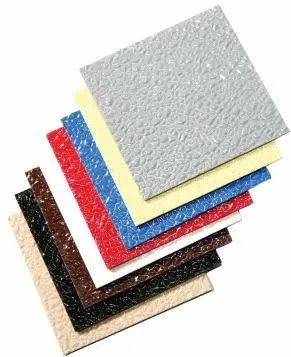
FRP panel manufacturers produce flat and lightly profiled sheet panels used as partitions, enclosure covers, cladding, machine guards, false ceiling panels and equipment housings. Unlike a single-purpose product line, panel fabricators often run varied panel sizes, thicknesses and finishes through the same production line to serve different customer specifications.
Why GP Clear Resin is suitable
Running varied panel work through one production line means the resin itself needs to be the constant — the same viscosity, gel time and cure behaviour regardless of which panel is being laminated that day. GP Clear Resin's 350–450 cPs viscosity and sub-8-minute gel time give panel fabricators that predictability, wetting out reinforcement evenly whether the mould is a large partition sheet or a smaller enclosure cover. Its non-accelerated cure system means dosage can be adjusted panel to panel without switching resin grades, which keeps a mixed-panel production line simple to run.
Required resin characteristics
- 01Predictable viscosity and gel time across varied panel sizes and thicknesses
- 02Even wet-out on both flat and lightly profiled panel surfaces
- 03Adjustable cure speed to match differing batch sizes without changing resin grade
- 04Adequate mechanical strength for panels used as partitions, guards and enclosure covers
- 05Batch consistency so panel quality doesn't vary as production shifts between different jobs
Manufacturing process
Panels are laminated by hand lay-up over flat or profiled moulds: chopped strand mat is wet out with resin catalysed by an MEKP hardener and cobalt octoate accelerator, rolled to remove air and achieve even thickness, then left to cure at room temperature. Panel thickness and reinforcement layers are adjusted to the specific job — a lightweight ceiling panel needs far less laminate than a structural enclosure cover — before trimming, drilling and any edge-finishing required.
Advantages
- Fast gel time supports efficient turnaround across a mixed-panel production schedule
- Non-accelerated cure system adapts to different batch sizes without a resin change
- 225 kg drum packaging suits continuous, varied panel production
- Consistent 99% purity keeps quality uniform across every panel type run through the line
Common products produced
- Toilet cubicle and partition panels
- Electrical enclosure and machine guard covers
- Wall cladding and false ceiling panels
- Equipment housings and general FRP sheet products
Frequently asked questions
Yes. Its predictable viscosity and gel time make it suitable across varied panel jobs — fabricators adjust laminate thickness and reinforcement layers per panel rather than switching resin grades.
Yes. FRP Polyester Pigment can be blended into GP Clear Resin before catalysing to produce coloured panels for cladding or décor applications, in addition to a clear or natural finish.
E-glass chopped strand mat is the standard reinforcement, with layer count adjusted to the mechanical demands of the specific panel — a lightweight ceiling panel needs less than a structural enclosure cover.
It is cured at room temperature with an MEKP catalyst (around 1.5%) and a cobalt octoate accelerator (around 0.4%), with dosage adjusted to the batch size and pace of a given production run.
GP Clear Resin is a standard general-purpose resin without fire-retardant additives. Where a panel needs a fire-rating specification, Samrat Poly Resins' Fire Retardant Resin is the more suitable choice.
Need resin for your FRP panel production?
Get a bulk quote or talk to our technical team about the right grade and dosage for your panel fabrication line.