Terephthalic DMC Resin
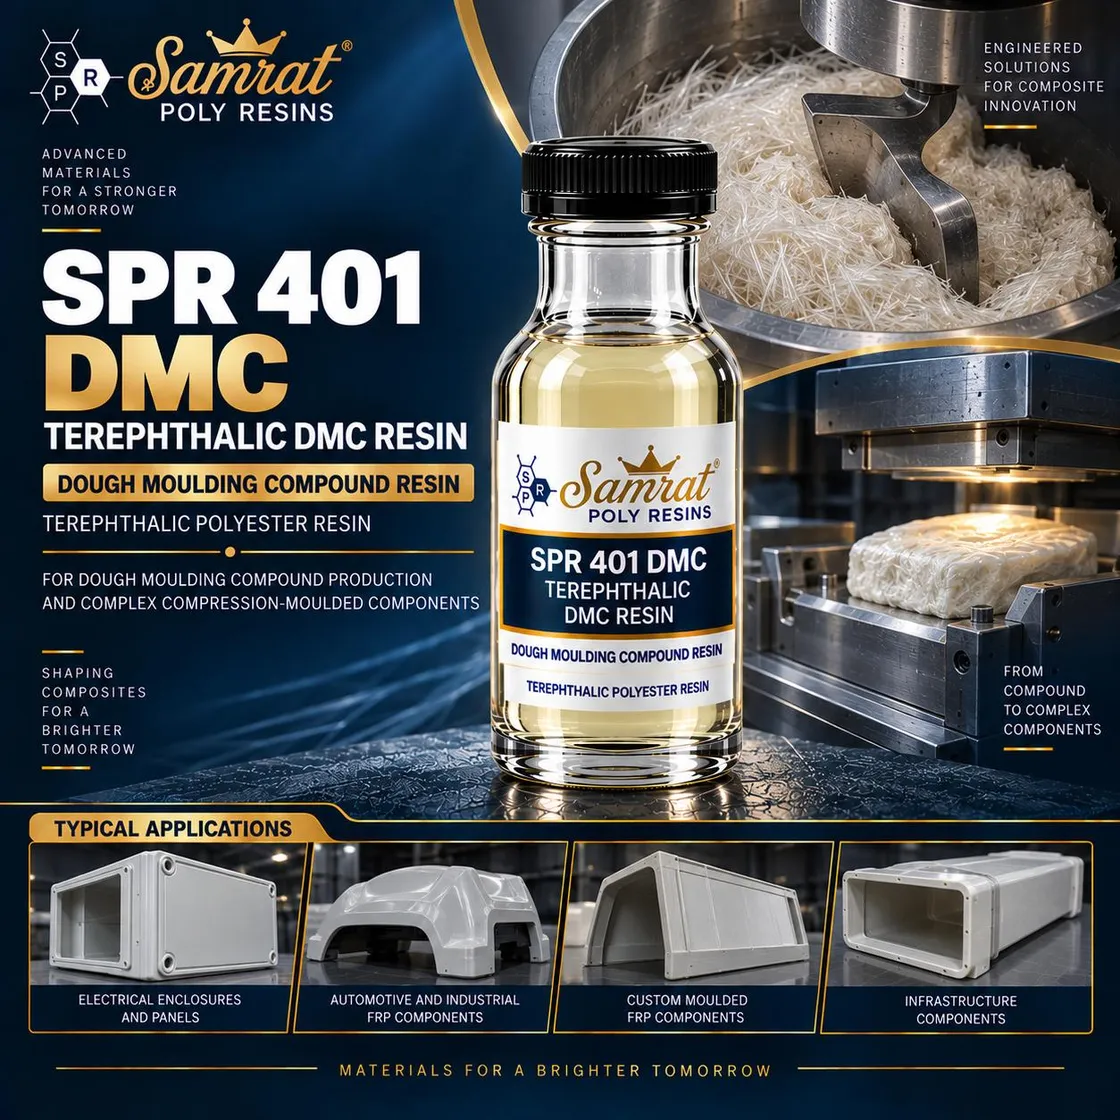
SPR 401 DMCTerephthalic dough moulding compound resinSPR 401 · Terephthalic Polyester Resins
Terephthalic resin for dough-moulding-compound production, with its own specification.
Review the official product data sheet for specifications and application information.
Price
Price on Request
Industrial resin pricing varies based on:
- Order Quantity
- Resin Grade
- Current Raw Material Rates
Product details
| Catalogue Code | SPR 401 DMC |
|---|---|
| Resin Chemistry | Terephthalic unsaturated polyester |
| Compound Type | Dough moulding compound (DMC) |
| Supply Condition | Non-accelerated |
| Reference Cure System | MEKP 1.5% + Cobalt Octoate 0.5% — added separately during use |
Typical specification
| Appearance | Clear to light-yellow liquid |
|---|---|
| Viscosity | 1,200–2,200 cPs at 25 °C |
| Gel Time | 14–22 minutes at 25 °C (ambient QC) |
| Specific Gravity | 1.11–1.15 |
| Styrene Content | 31–36% by weight |
Typical values from the Samrat Poly Resins product catalogue, 2026 edition. They are not guaranteed specifications or finished-component properties; confirm the current values for your order and trial the grade on your own process.
SPR 401 DMC is the terephthalic dough moulding compound resin of the SPR 401 family — a separate product from the SMC resin, with its own specification. It is listed for dough moulding compound production, compression-moulded composite components and complex moulded FRP parts, and is supplied non-accelerated, with MEKP and cobalt octoate at 0.5% added separately during use.
The terephthalic sheet moulding compound resin is Terephthalic SMC Resin. DMC resins in the other families: Isophthalic DMC Resin and the orthophthalic DMC/SMC Resin.
Key features
- Terephthalic resin for dough moulding compound (SPR 401 DMC)
- Its own specification, separate from the SMC resin
- Typical viscosity 1,200–2,200 cPs; ambient QC gel time 14–22 minutes at 25 °C
- Reference cure system uses cobalt octoate at 0.5%
Applications
- Dough moulding compound production
- Compression-moulded composite components
- Complex moulded FRP parts
Product role
Unlike the isophthalic pair, the terephthalic SMC and DMC resins carry different specifications in the catalogue: the DMC resin is more viscous (1,200–2,200 cPs against 800–1,500 cPs) with a slightly longer ambient gel time. They are separate products, not variants of one grade.
Compound formulation and moulding conditions belong to the compounder. Share the compound type, the moulded part and any governing specification when enquiring.
Supply and cure
- Supply condition
- Non-accelerated
- Reference cure system
- MEKP 1.5% + Cobalt Octoate 0.5% — added separately during use
Processes and where this grade fits
SPR 401 DMC is the terephthalic dough moulding compound resin, more viscous than its SMC counterpart, for compression-moulded and complex moulded parts.
| Process or use | Role of this grade | What to confirm |
|---|---|---|
| DMC / BMC dough mixing | Listed role | Filler loading, fibre length and dough handling |
| Compression moulding of DMC components | Listed role | Tool temperature and press cycle |
| Complex moulded FRP parts | Listed role | Flow into ribs, bosses and inserts |
| SMC sheet production | Consider SPR 401 SMC | The separate terephthalic SMC resin |
Process-selection considerations
- The terephthalic SMC and DMC resins carry different specifications: the DMC resin is more viscous, 1,200–2,200 cPs at 25 °C typical, with a slightly longer ambient gel time of 14–22 minutes at 25 °C.
- Choose the family by what the moulded part requires, not by name.
- Its reference QC cure uses more cobalt octoate than the SMC resin: MEKP 1.5% with cobalt octoate 0.5%, added separately.
- Share the part geometry: complex parts with ribs and bosses test compound flow.
- Describe the compound formulation principles and any storage requirement for the dough.
Limitations and trial requirements
- No moulded-part mechanical, electrical or heat values are published for SPR 401 DMC.
- Ambient gel time is a QC figure; hot-mould cure belongs to the compound.
- The terephthalic family description in the catalogue is qualitative; it is not a numerical property of this grade.
- Trial the grade on the real part, mould and shop conditions before production. The catalogue values are typical liquid-resin properties, not guaranteed limits or finished-part performance.
Before you select this grade
- The values on this page are typical. Final selection should be confirmed against your own process, a trial result and the current technical documentation for the grade.
- The Technical Data Sheet linked on this page carries these same typical values. No Safety Data Sheet is published on this site for this grade; request current safety information before use.
- Never mix a concentrated peroxide initiator directly with a cobalt accelerator. Add each to the resin separately, according to the confirmed process.
- Store resin, initiators and accelerators separately, in original sealed containers, cool, shaded and away from heat and ignition sources. Use suitable personal protective equipment and adequate ventilation.